Built for pharmaceutical manufacturing excellence
A 25,000 sq. ft. cGMP-compliant facility supported by 50+ skilled professionals, spanning production, laboratory, quality control and packaging.
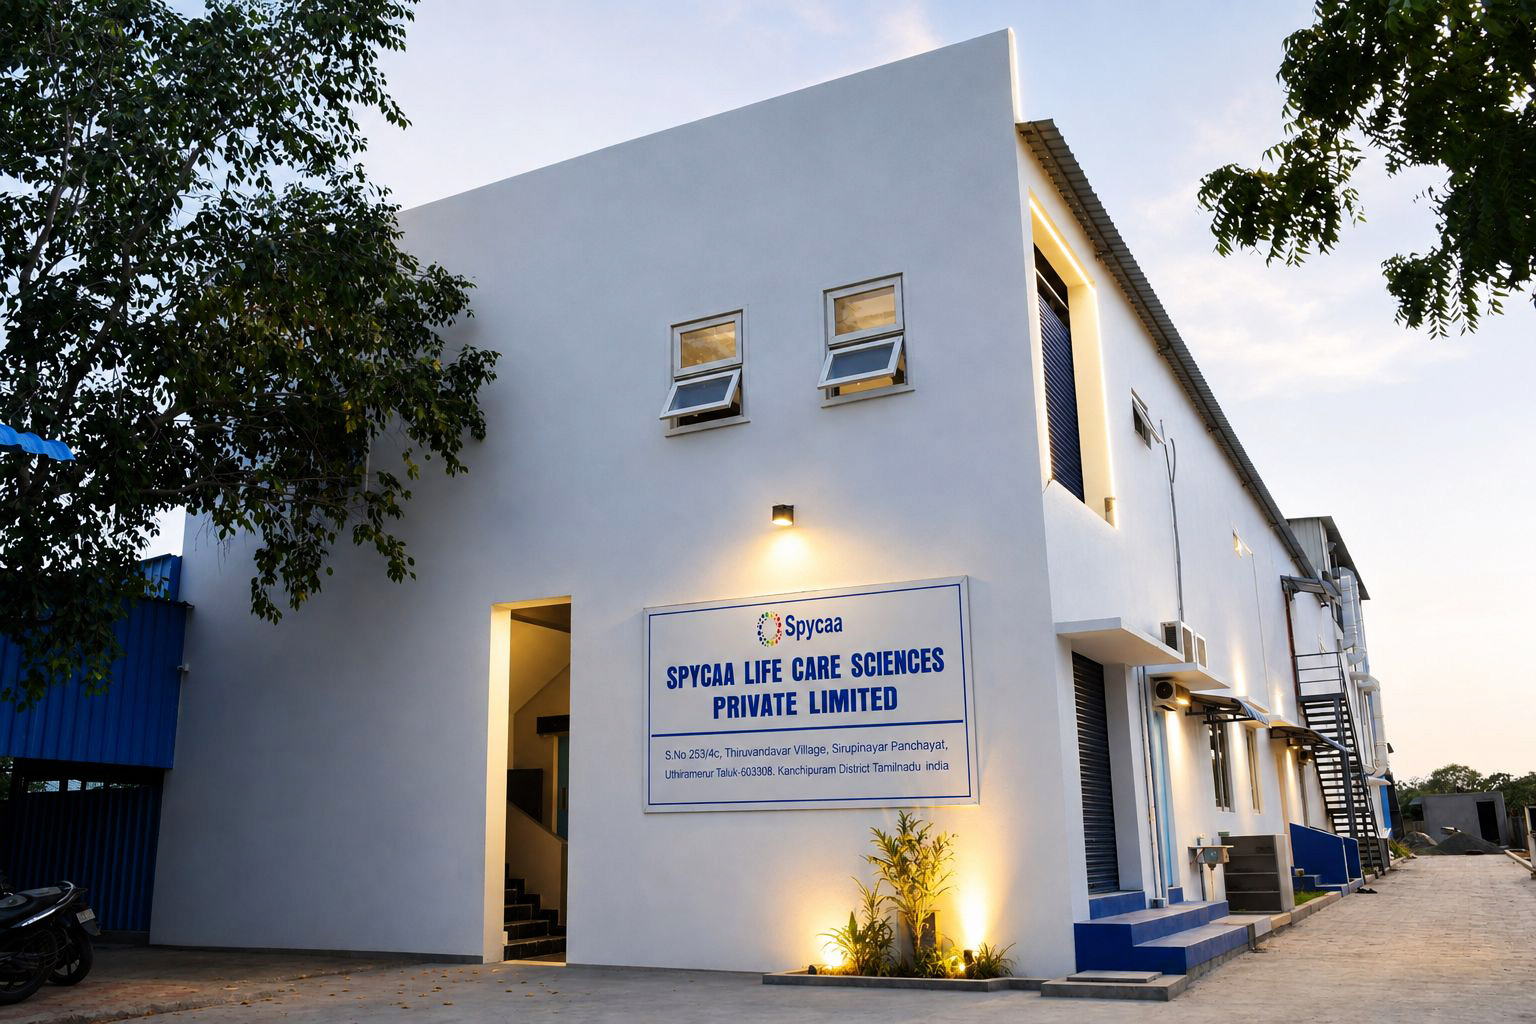
Manufacturing Area
Our 25,000 sq. ft. manufacturing facility is a spacious, well-equipped production area designed to support efficient pharmaceutical and nutraceutical manufacturing. With dedicated processing, production and packing spaces, it provides ample capacity for streamlined operations, quality control and scalable production, supported by a dedicated team of 50+ skilled professionals.
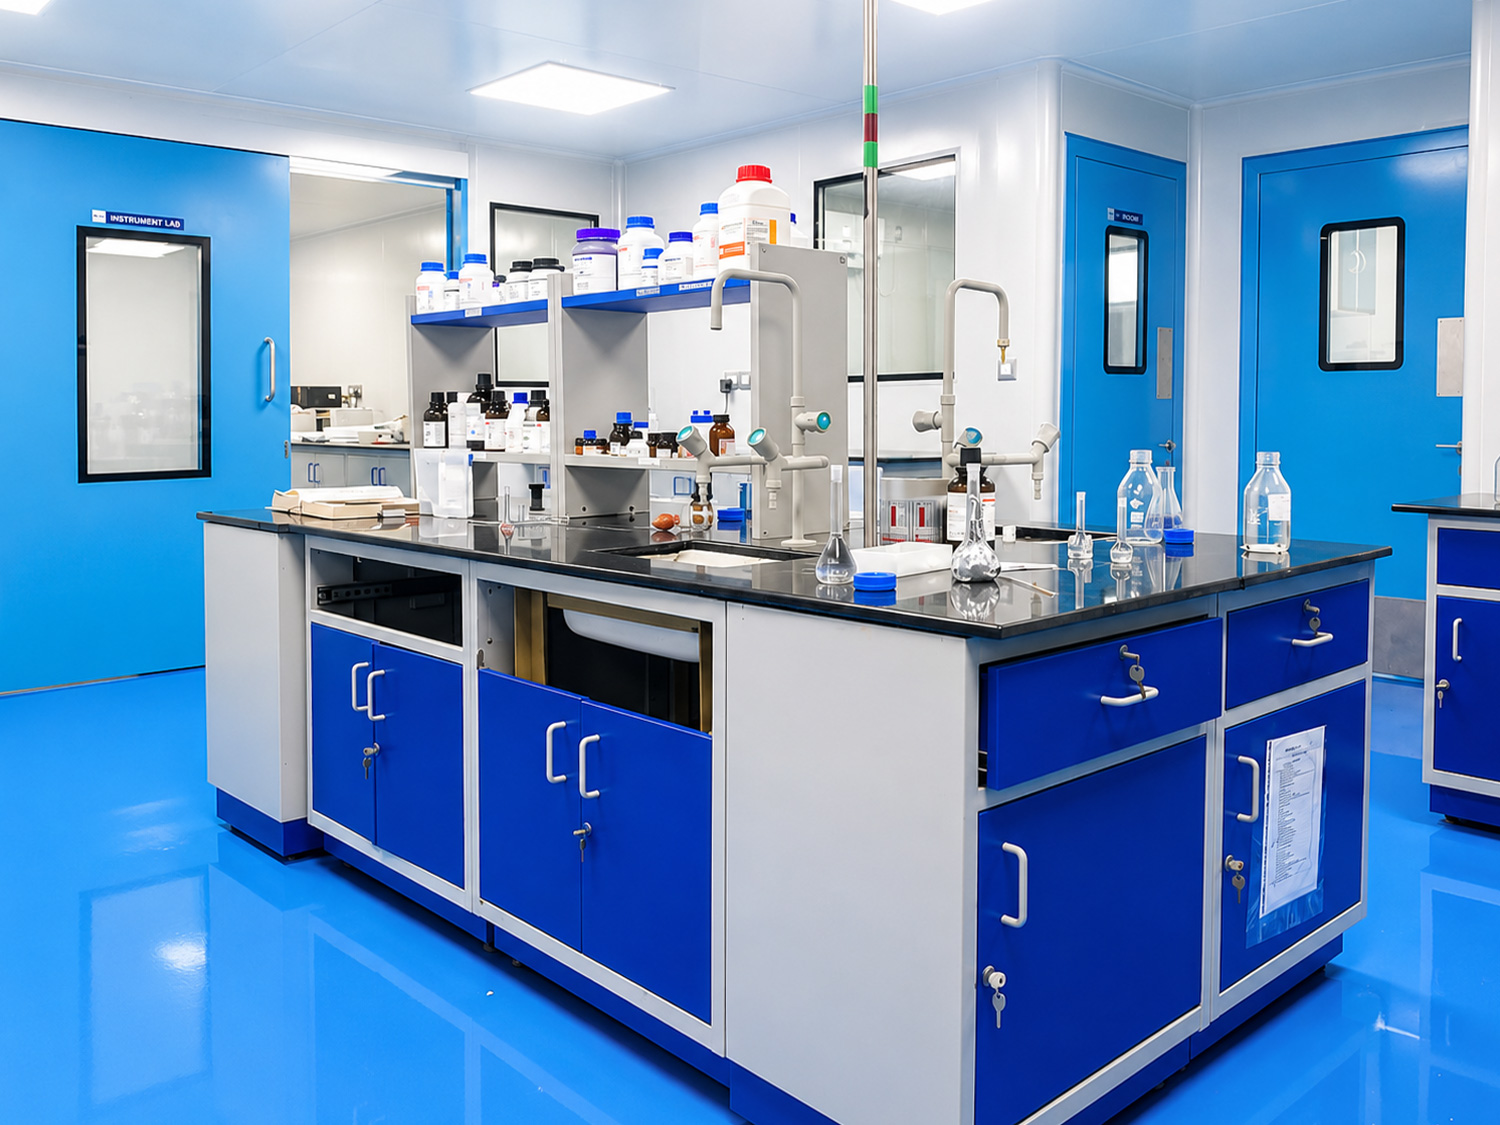
Advanced Laboratory Facility
Our well-equipped laboratory supports comprehensive testing, analysis and quality evaluation throughout the manufacturing process. Designed with a strong focus on accuracy, hygiene and controlled testing environments, it enables reliable assessment of raw materials, in-process samples and finished products, strengthening product consistency and safety.
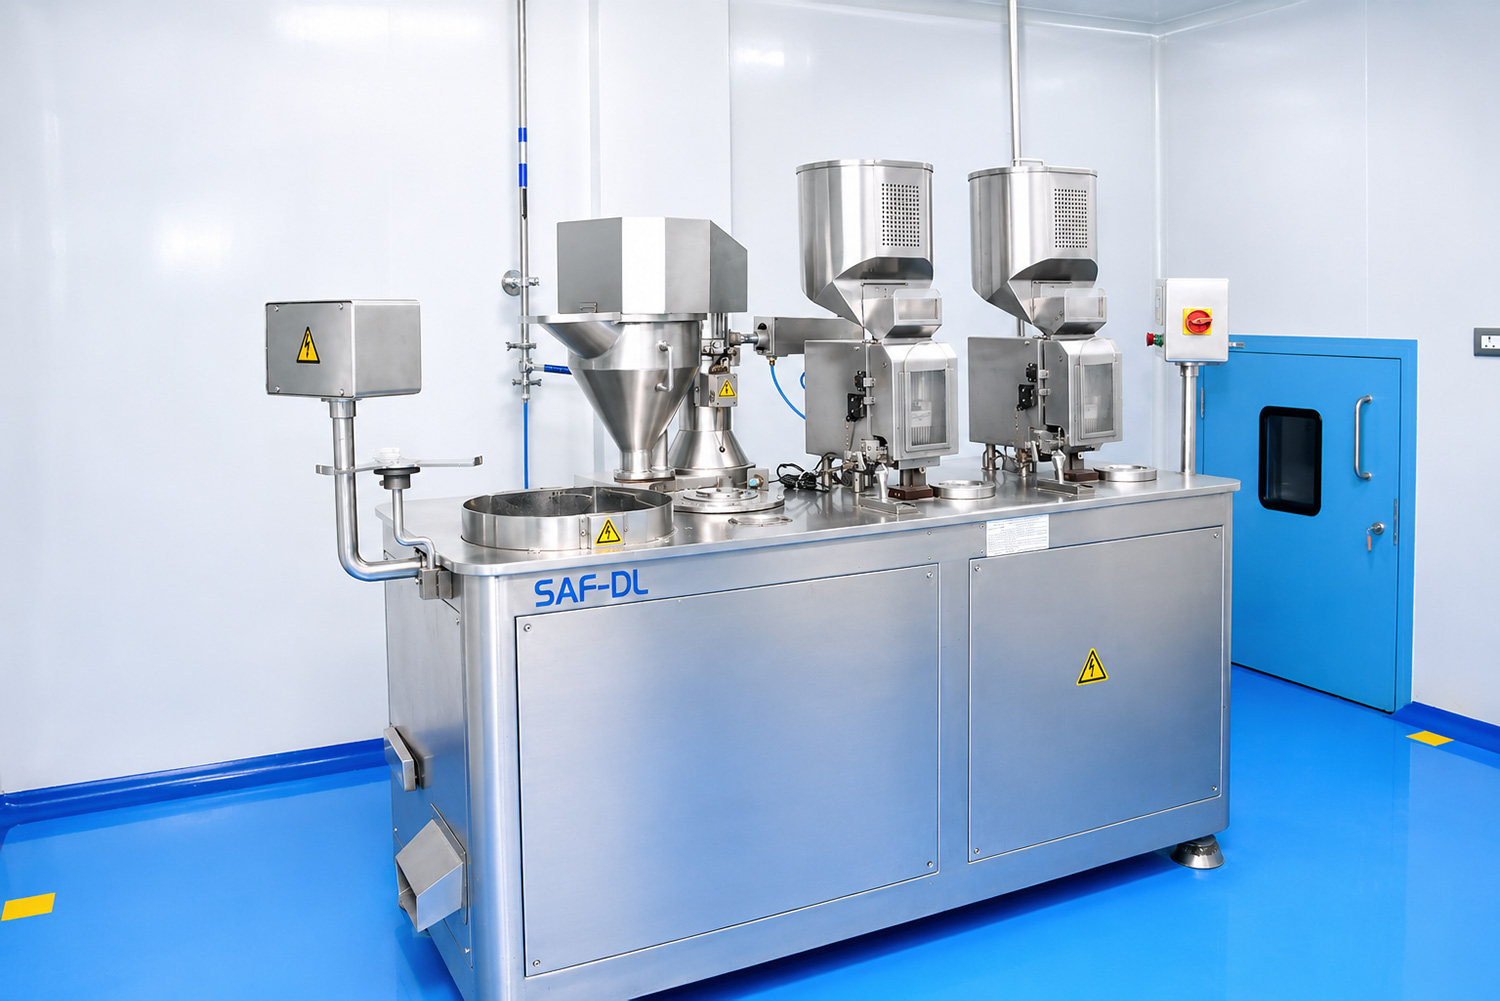
Advanced Capsule Filling Facility
Our advanced capsule filling facility is equipped with precision-engineered machinery for efficient, accurate and hygienic capsule production. With a focus on consistency, quality and operational excellence, the system enables reliable filling while supporting high manufacturing standards and scalable capacity.
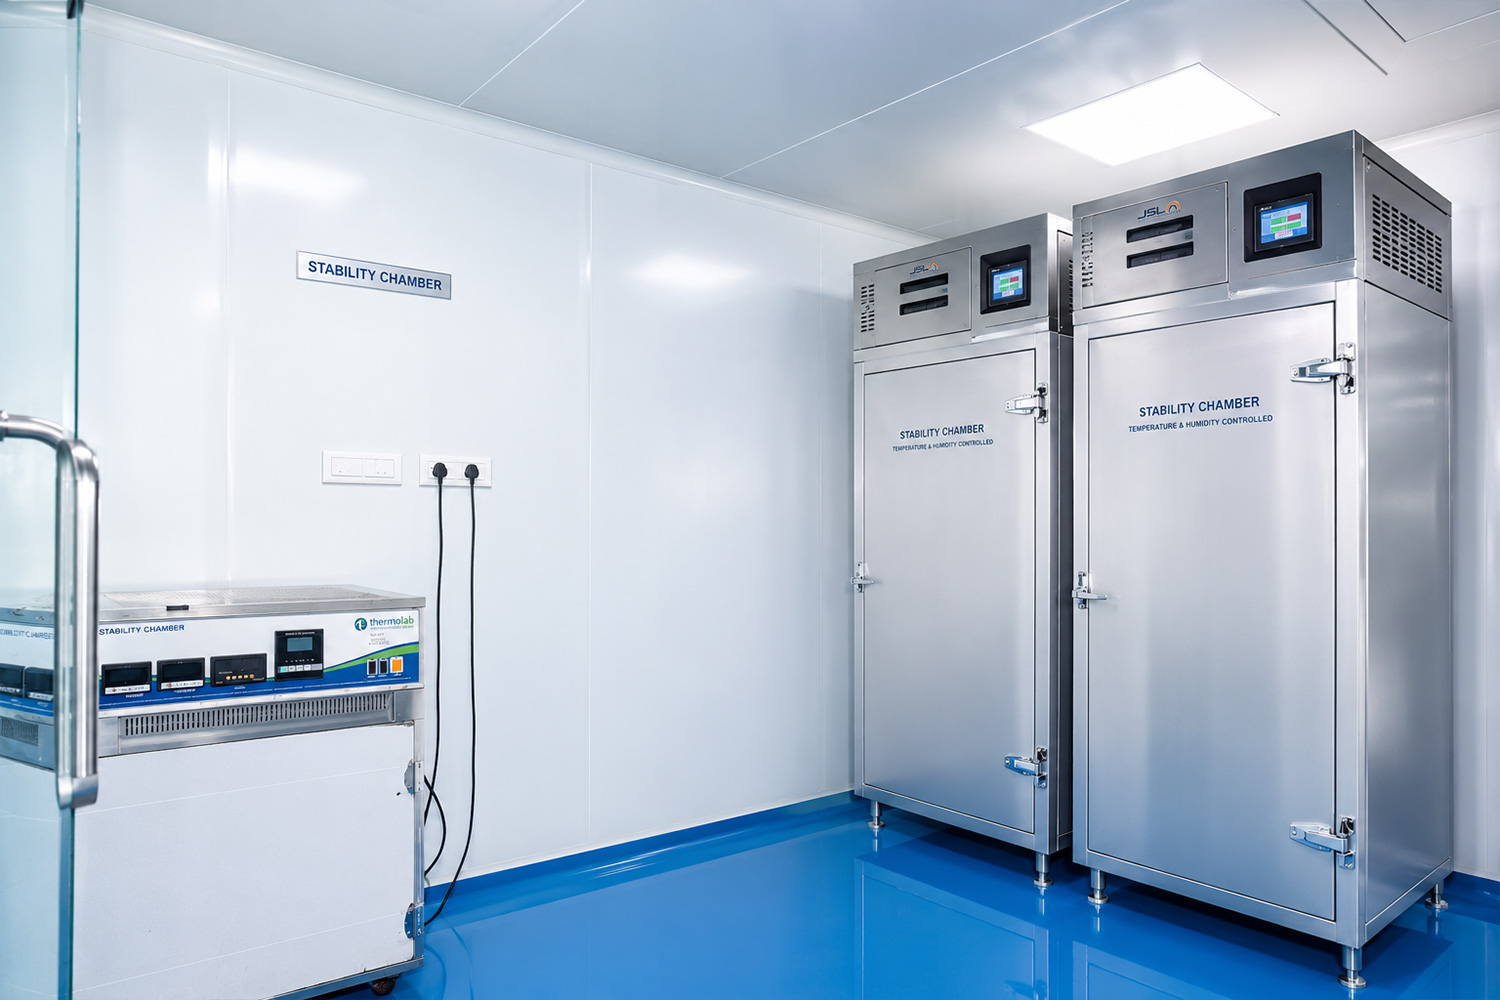
Stability Chamber
Our pharmaceutical stability chamber maintains precise temperature and humidity parameters for evaluating the stability and quality of products. It supports stability studies and helps assess product performance throughout the intended shelf life, reflecting our commitment to quality and compliance.
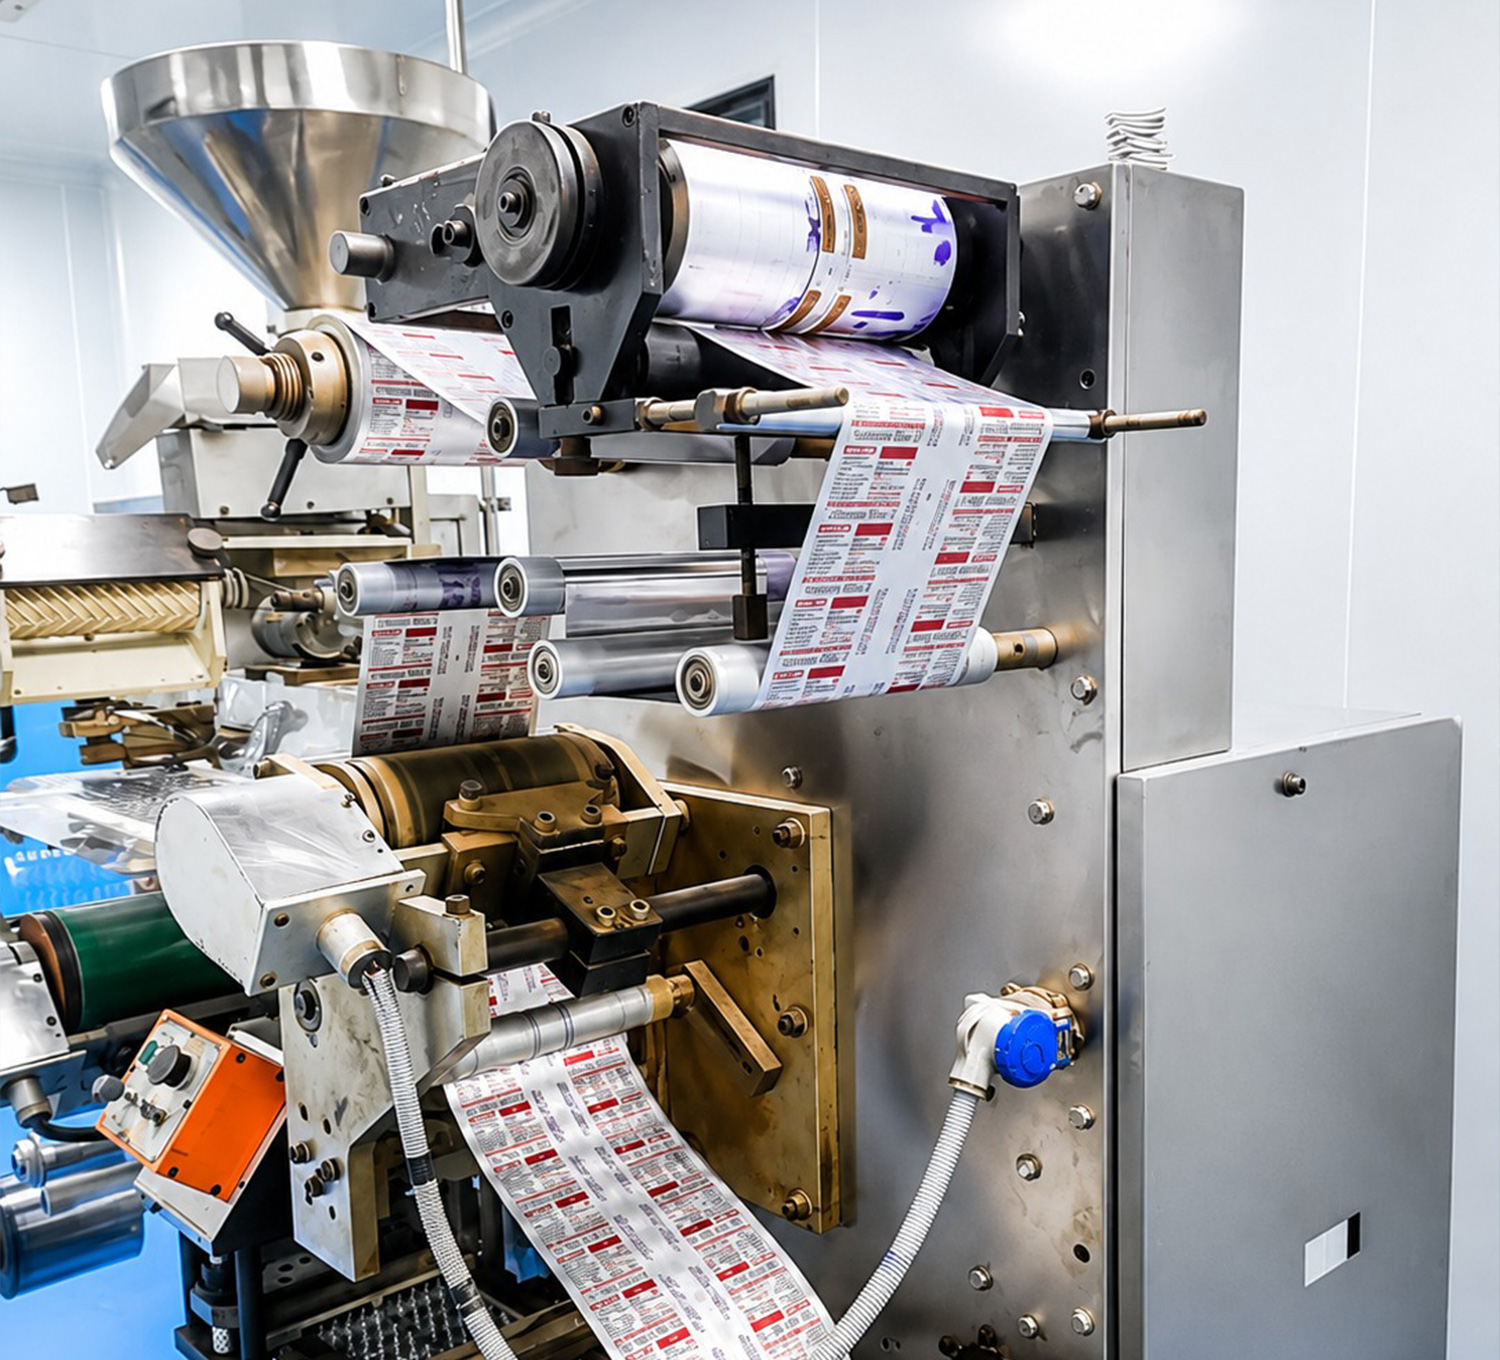
Advanced Packaging Machine
Our advanced packaging facility is equipped with efficient machinery for accurate, hygienic and reliable product handling. The system ensures consistent packaging quality while supporting operational efficiency and product protection throughout the final stage of manufacturing.
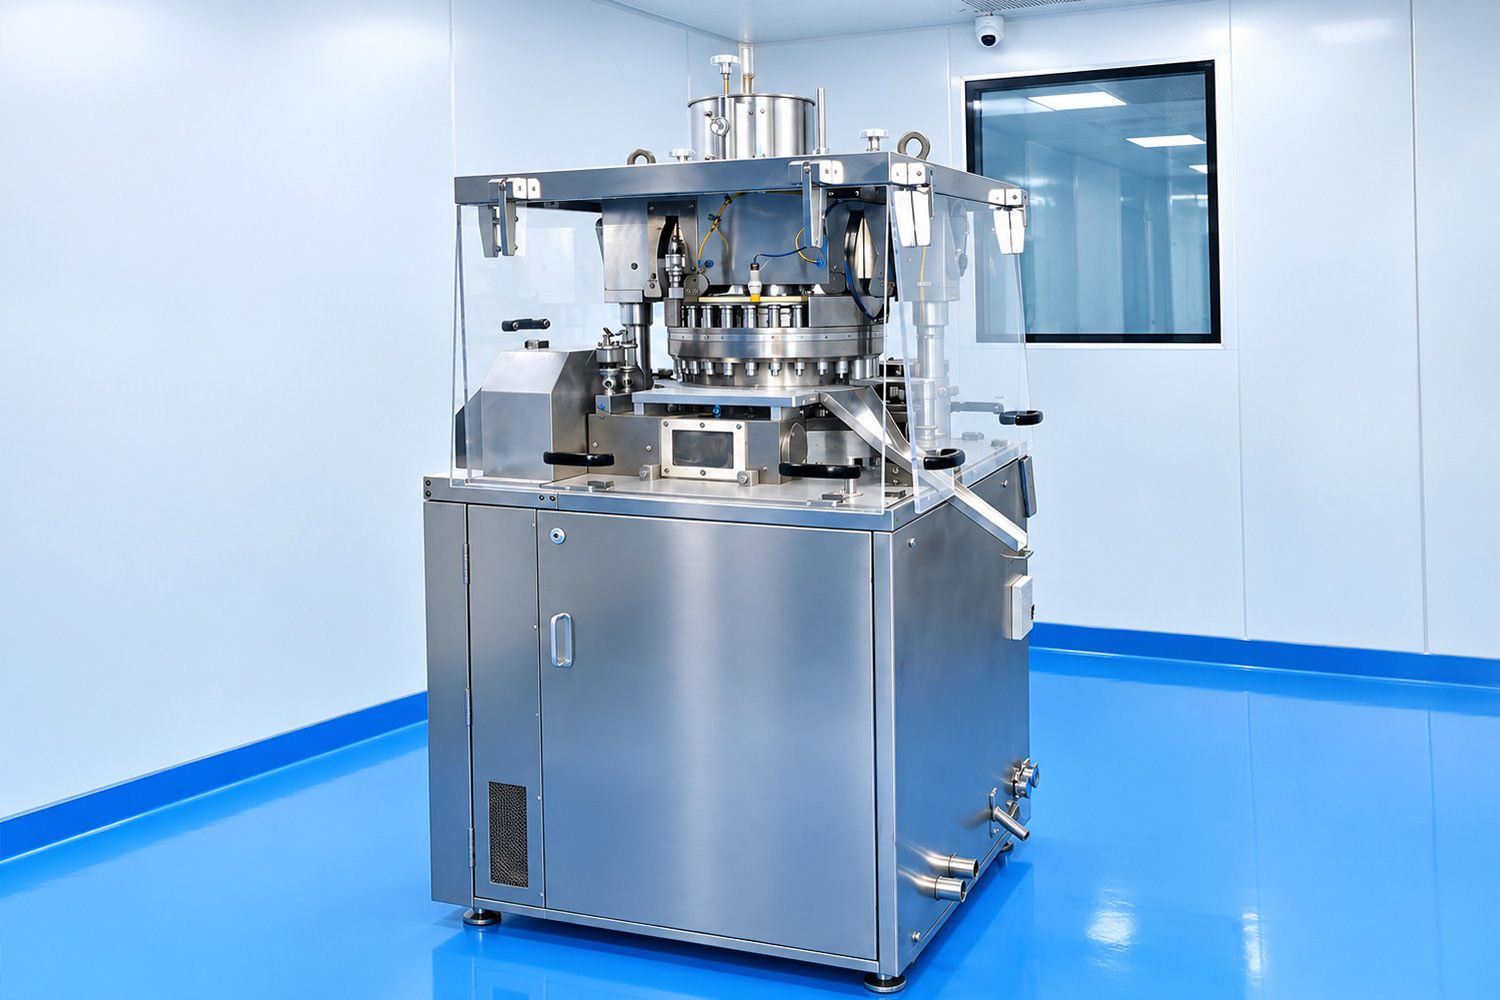
Tablet Compression Machine
Our advanced tablet compression facility uses precision-engineered machinery for consistent, efficient and reliable tablet manufacturing. It supports accurate compression, uniform tablet weight and consistent product quality while maintaining high standards of hygiene and process control.
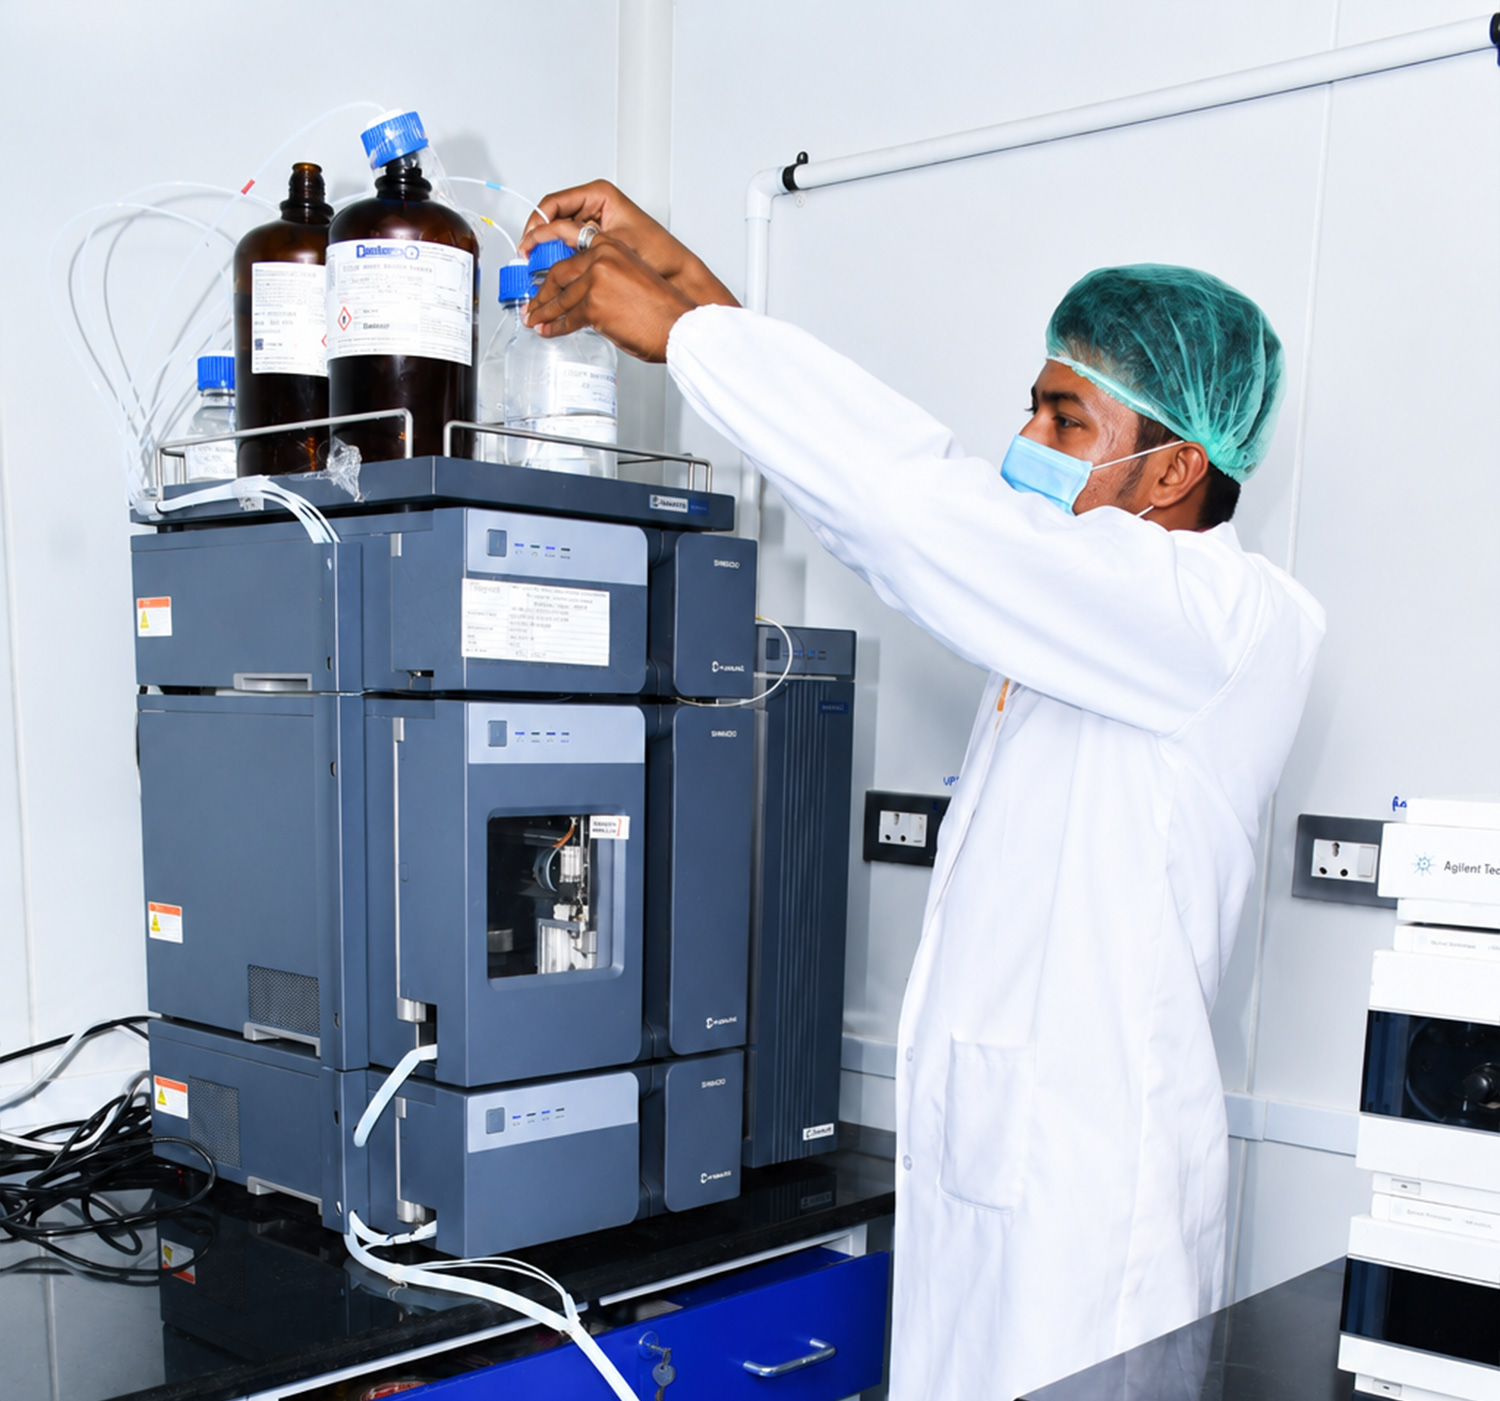
High-Performance Liquid Chromatography (HPLC)
Our advanced HPLC facility supports precise analytical testing and quality evaluation of products and raw materials. Equipped for accurate identification, quantification and purity analysis, it enables reliable assessment of critical quality attributes throughout the manufacturing process.
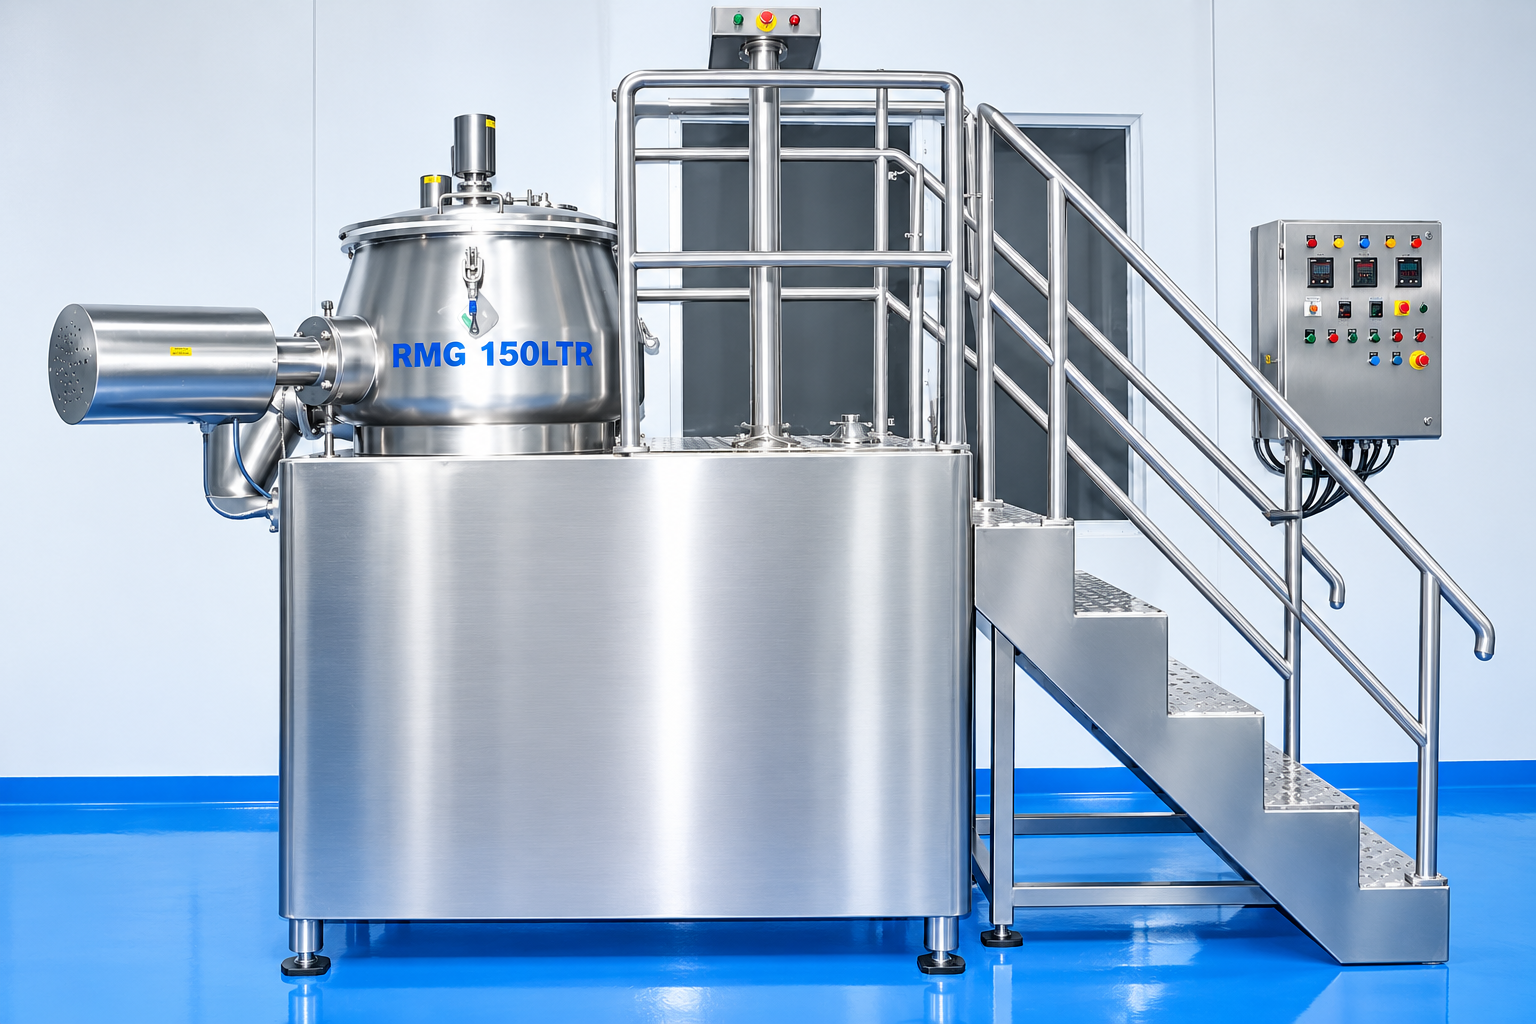
Rapid Mixer Granulator (RMG)
Our Rapid Mixer Granulator (RMG) facility is designed to support efficient and controlled wet granulation processes for pharmaceutical manufacturing. The system enables uniform blending, precise binder incorporation and consistent granule formation, ensuring improved process control, product uniformity and batch-to-batch consistency. With a focus on hygiene, operational reliability and GMP-oriented manufacturing practices, our facility supports high-quality pharmaceutical production while maintaining stringent process and quality standards.
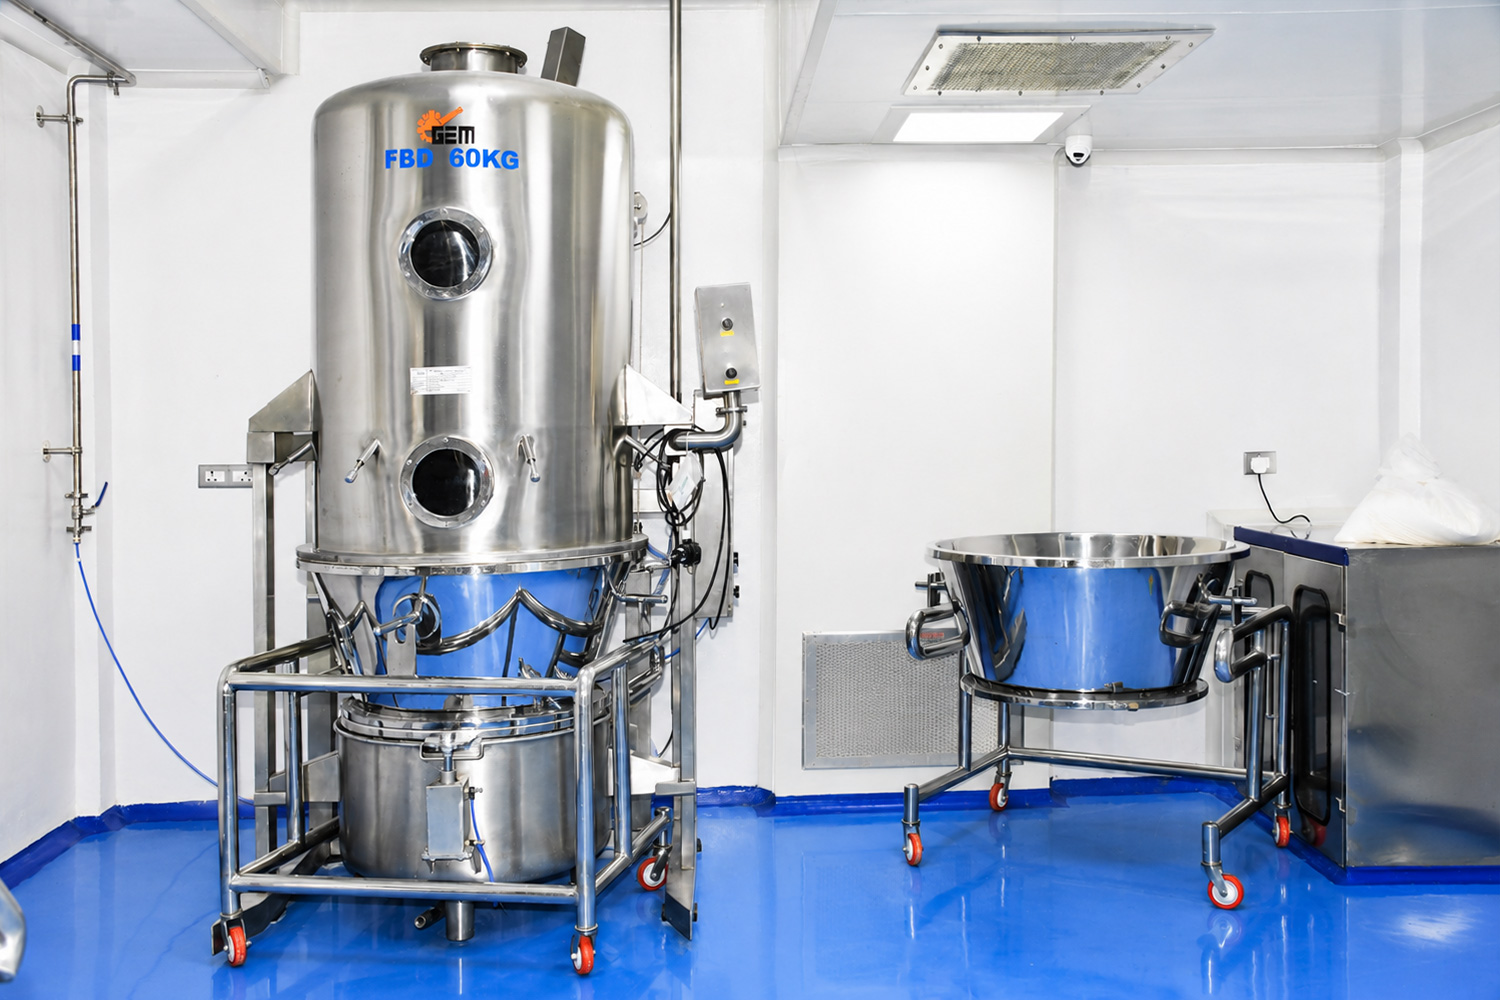
Fluid Bed Dryer (FBD)
Our Fluid Bed Dryer (FBD) is an advanced pharmaceutical processing system engineered to deliver efficient, uniform and controlled drying of pharmaceutical granules and powders. Designed with a focus on process consistency, hygiene and operational reliability, the system enables precise control of airflow and temperature to achieve optimal moisture levels and product quality. Its robust construction and controlled drying environment support efficient batch processing while aligning with the stringent quality and manufacturing standards of the pharmaceutical industry.
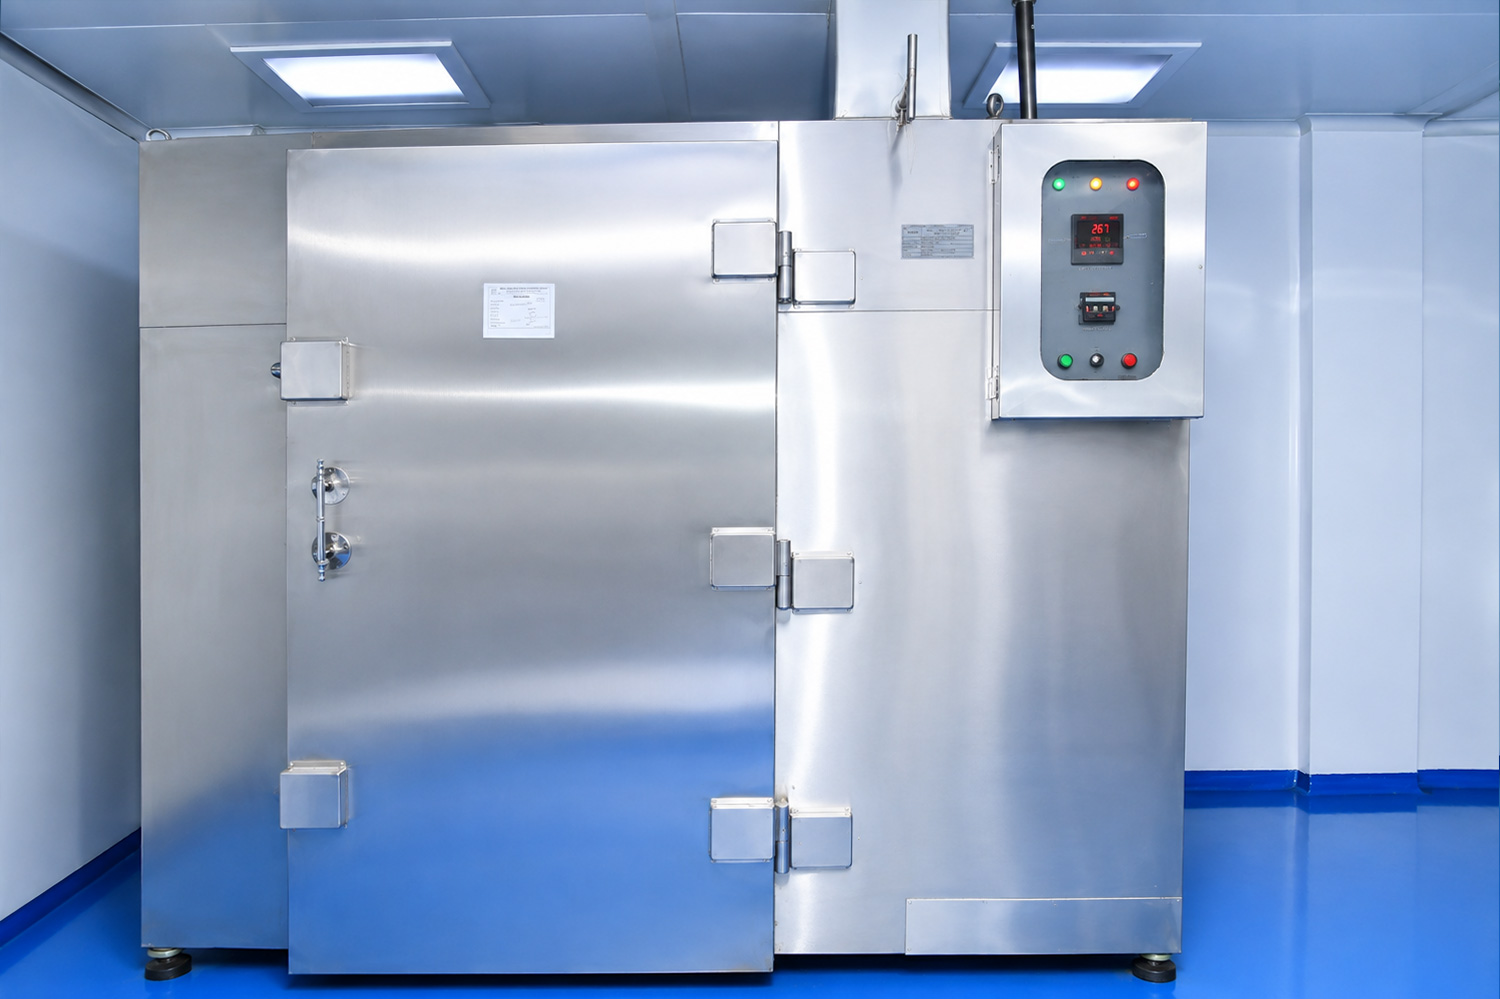
Tray Dryer
Our pharmaceutical-grade tray dryer provides controlled, uniform drying of powders, granules and other formulations. Efficient heat distribution and controlled drying conditions support consistent moisture removal while maintaining product quality across diverse product requirements.
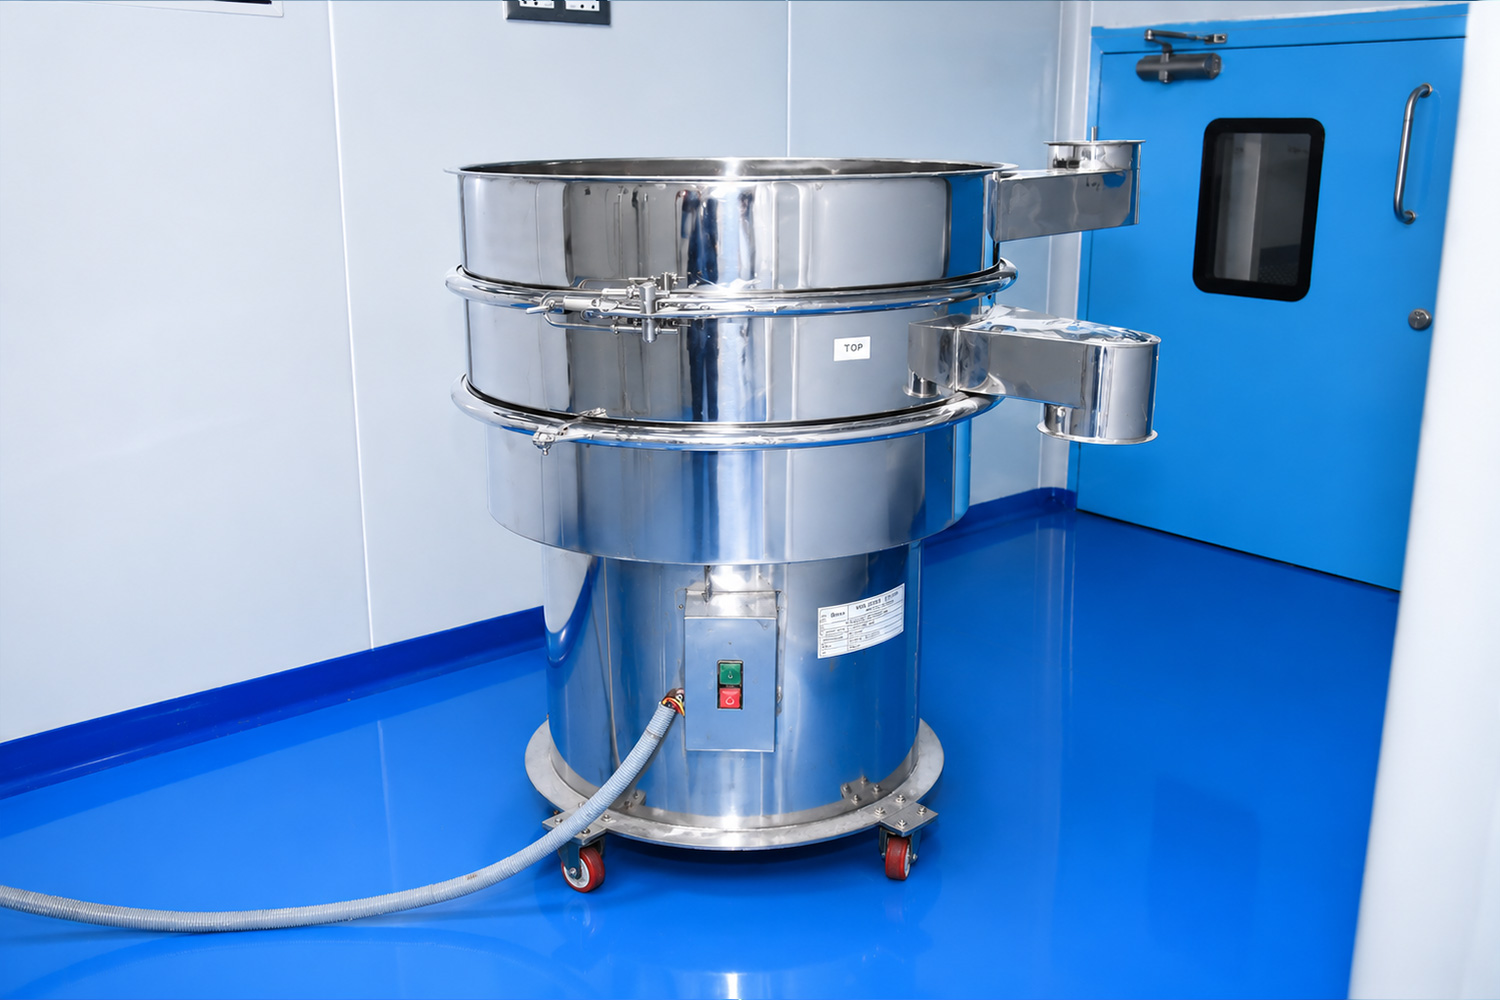
Pharmaceutical Sifter
Our pharmaceutical-grade sifting equipment provides efficient, uniform separation of powders and granules to achieve the desired particle size and consistency. It supports effective removal of unwanted particles and smooth material flow for subsequent manufacturing processes.
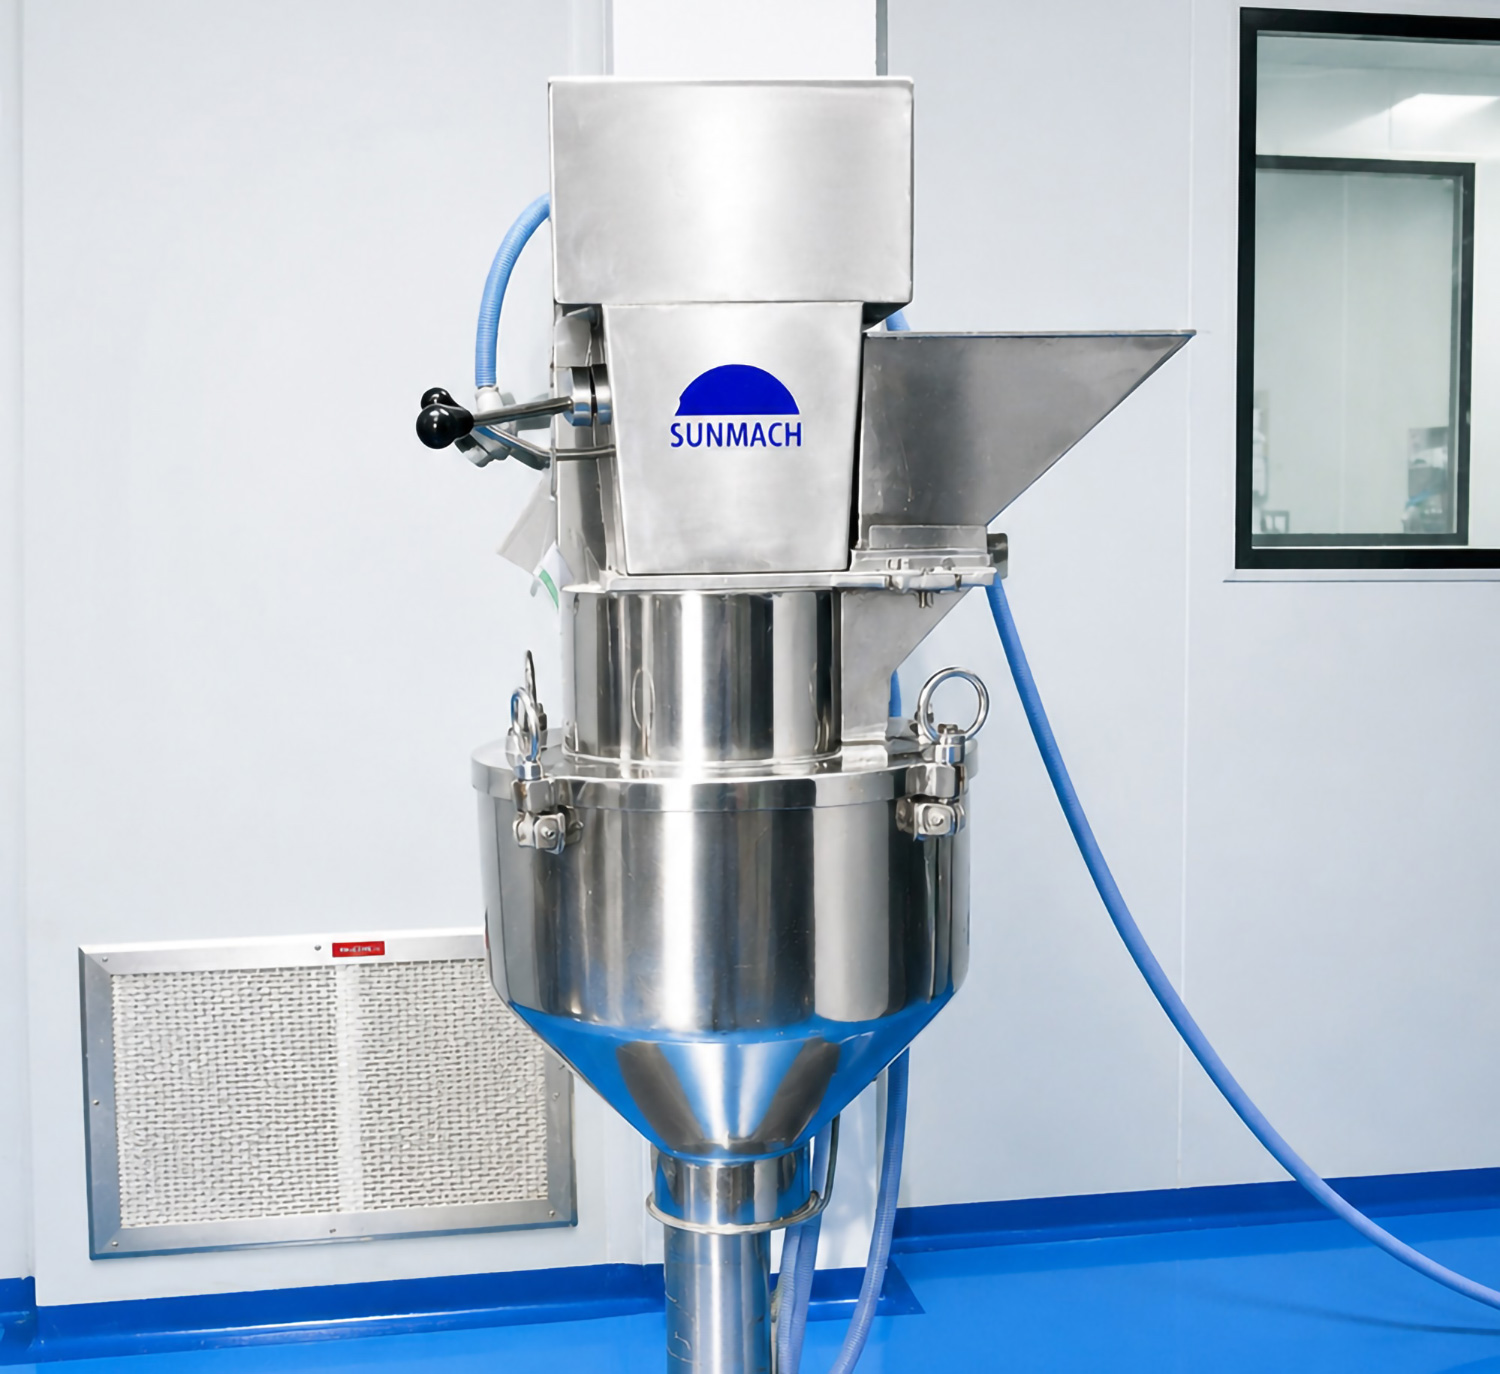
Pharmaceutical Milling Machine
Our advanced milling machine supports efficient size reduction and uniform particle processing of powders, granules and raw materials. It delivers consistent particle-size distribution, improved material flow and enhanced product uniformity across manufacturing processes.
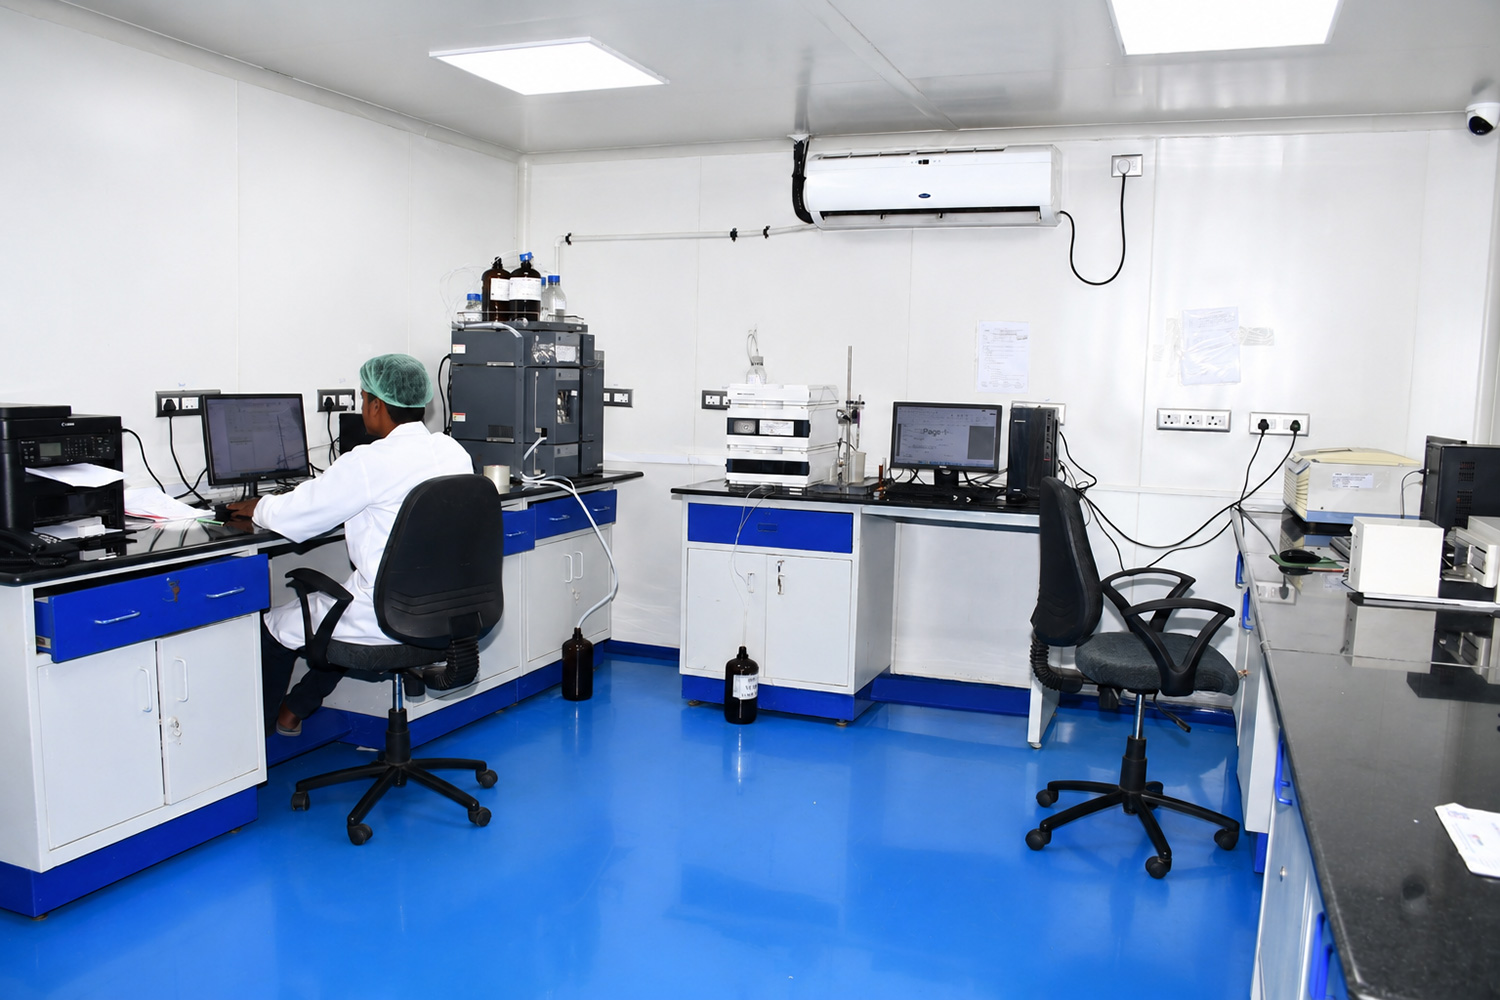
Quality Control (QC) Area
Our dedicated Quality Control facility supports comprehensive testing of raw materials, in-process materials and finished products. Equipped with advanced analytical instruments and controlled testing environments, it enables accurate, consistent and reliable quality assessment before every release.
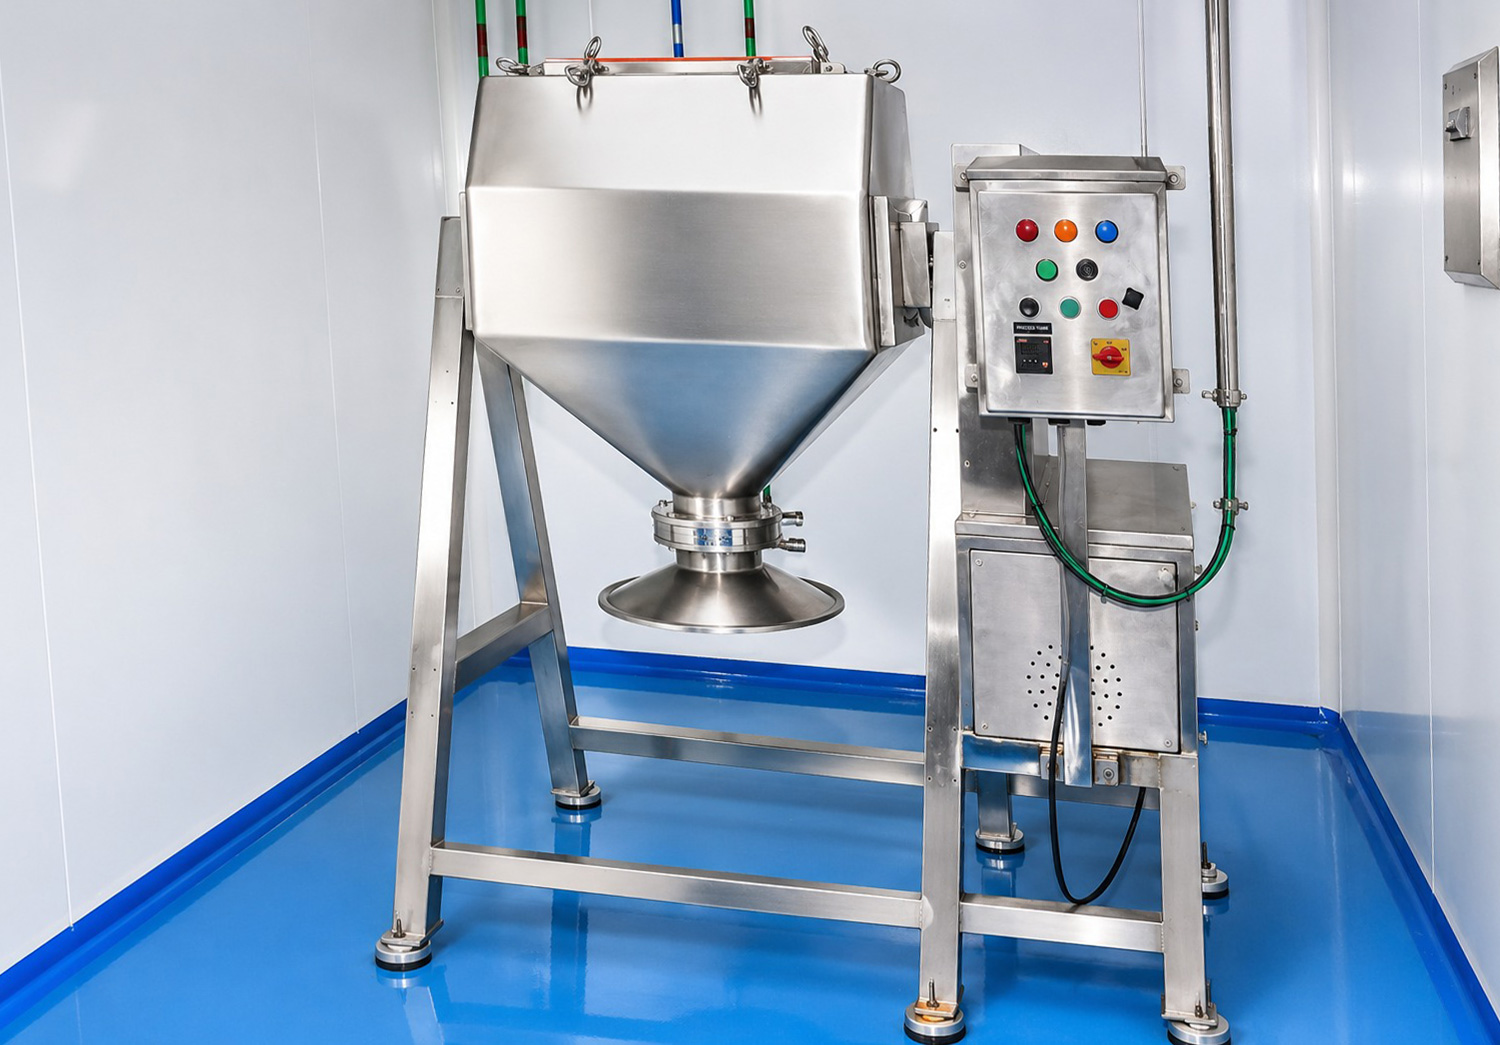
Pharmaceutical Blending Machine
Our advanced blending machine ensures efficient, uniform mixing of powders and granules, with consistent distribution of active ingredients and excipients throughout the formulation. It supports controlled blending, product uniformity and reliable batch-to-batch consistency.
Want to visit the facility?
Client audits and site visits are welcome. Get in touch to arrange a date.